Conveyor & Crane Modernization
Conveyor and crane modernization for aging equipment, controls, carriers, drives, runways, and support steel, with a scope shaped around the existing system.
Know who owns every interface.
Build the work around the site.
Agree what completion includes.
Bring clarity to the work.
Modernization Should Solve The Right Problem
Aging conveyors and cranes do not always need full replacement. Sometimes the right move is a targeted upgrade to controls, drives, carriers, hoists, support steel, runway, safety devices, or worn mechanical sections.
IMH reviews reliability issues, obsolete parts, chain stretch, worn track, trolley problems, drive overload, control gaps, production goals, and shutdown timing before recommending repair, retrofit, modernization, or replacement.
Modernization Targets
Track, chain, trolleys, carriers, hoists, runway components, and support steel may drive the scope.
Sensors, stops, switches, VFDs, panels, interlocks, and operator stations may need updates.
Modernization should support current products, flow, takt time, maintenance access, and future changes.
Repair, Retrofit, Or Replace
A good modernization conversation separates symptoms from root causes. A control issue may expose mechanical wear, and a mechanical issue may expose layout or maintenance-access problems.
IMH helps buyers evaluate what can stay, what should change, and what needs to be staged around production.
Modernization Review Inputs
These details help define whether upgrade, retrofit, repair, or replacement is the right path.
| Input | Why it matters |
|---|---|
| Problem history | Shows recurring downtime, maintenance issues, or performance limits. |
| Existing equipment | Identifies compatibility, parts, controls, and reusable structure. |
| Production goal | Clarifies whether the project needs throughput, reliability, safety, or flexibility. |
| Controls condition | Obsolete panels, sensors, drives, and operator stations may drive the scope. |
| Mechanical wear | Track, chain, wheels, runway, hoist, carriers, and support points need review. |
| Shutdown window | Defines phasing, preassembly, tie-ins, and startup. |
When To Modernize
Modernization makes sense when existing assets still have value but no longer support the plant well.
Modernization Should Improve The Future
A modernization project should not only get the system running again. It should make the next maintenance event, expansion, or product change easier.
IMH reviews access, structure, controls, and startup together so upgrades are not trapped inside the same old problems.
Should I repair or replace my system?
That depends on age, wear, parts availability, controls, structure, safety, and production goals.
Can IMH modernize conveyor controls?
IMH can review controls coordination as part of conveyor and system upgrade planning.
Can modernization be phased?
Often, yes. Phasing depends on compatibility, downtime, access, and startup requirements.
What information is needed?
Photos, drawings, problem history, parts history, controls photos, and production goals.
Does modernization include installation?
Installation and startup should be discussed as part of the modernization scope.
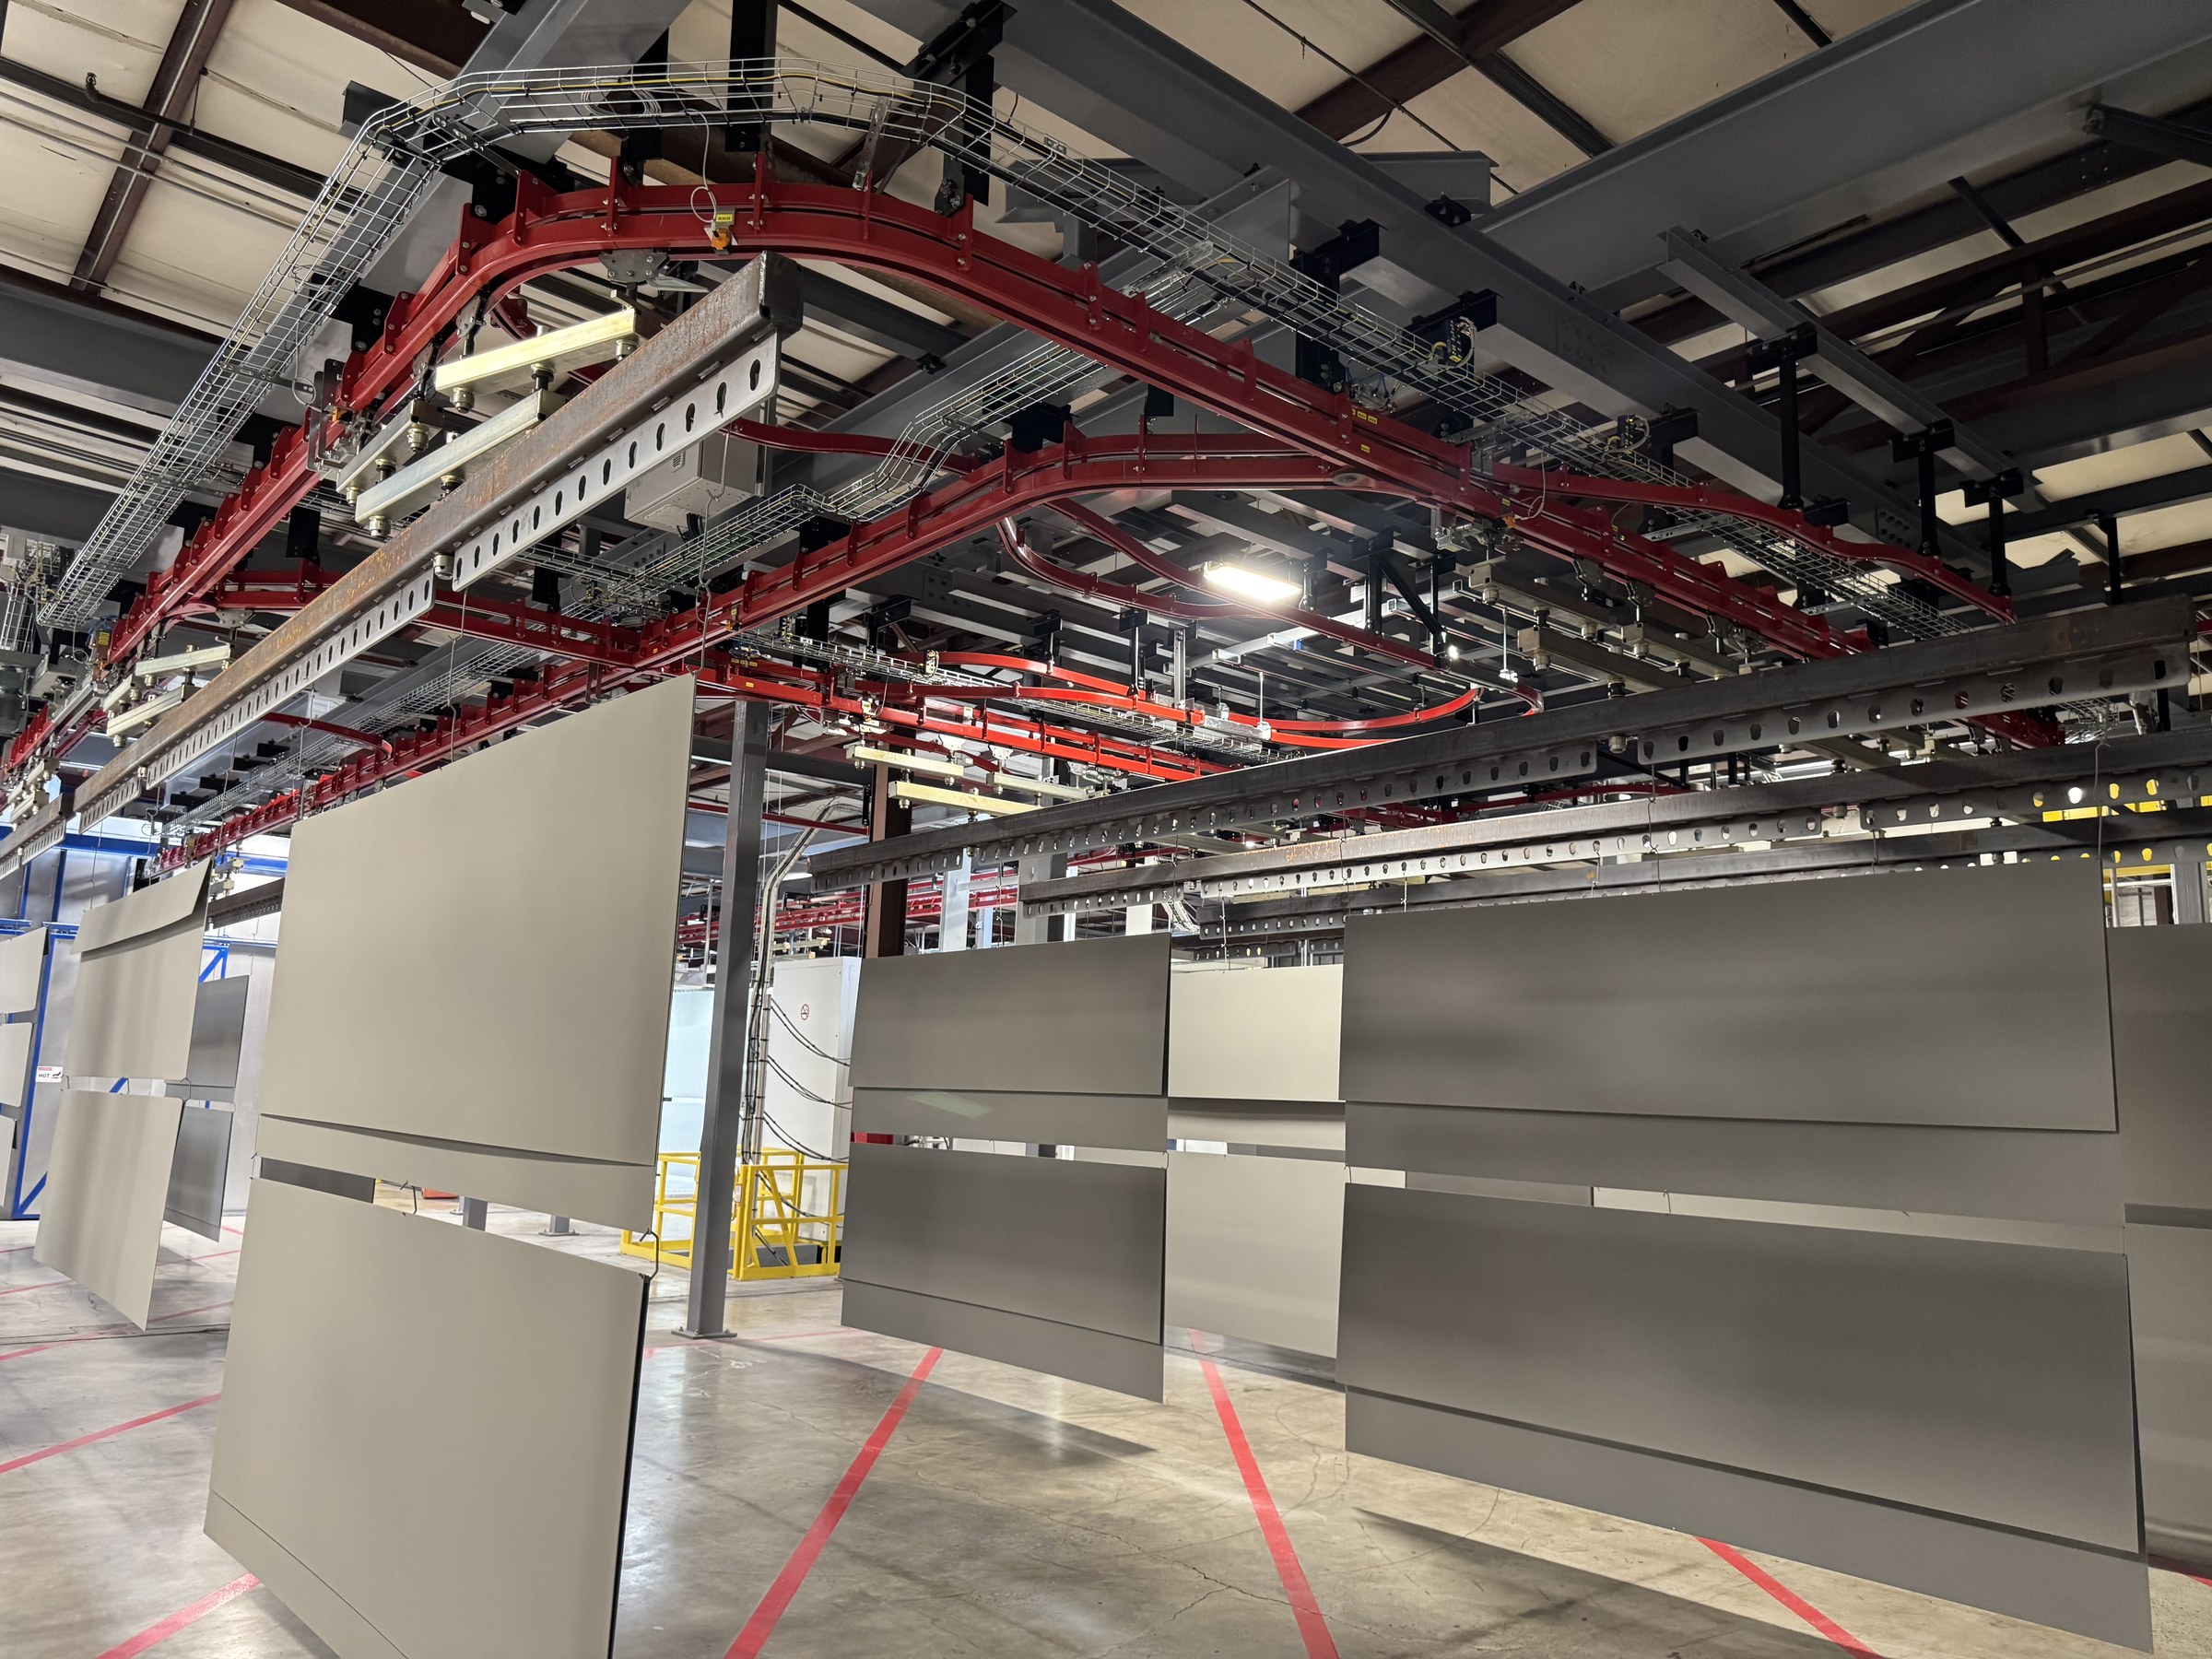
Power & Free. Installed for the Project Team.
Installation of a supplied power-and-free conveyor, with field layout coordination and overhead equipment integration in a finishing area.
- IMH responsibility
- Installation · design and equipment supplied by others
A field scope that fits.
Define delivery, access, assembly, utilities, and handover with the project team.
Tell us what
needs attention.
Share the equipment, symptoms, project location, and production impact. We’ll discuss the service scope and availability. For a time-sensitive need, call directly.
Discuss service Or call (812) 363-1819