Demand and takt
Required takt is available production time divided by required good-part demand. Specify whether breaks and planned stops are already removed from available time.
Translate production demand into equipment capacity, conveyor flow, and a realistic operating schedule.
Discuss your engineering project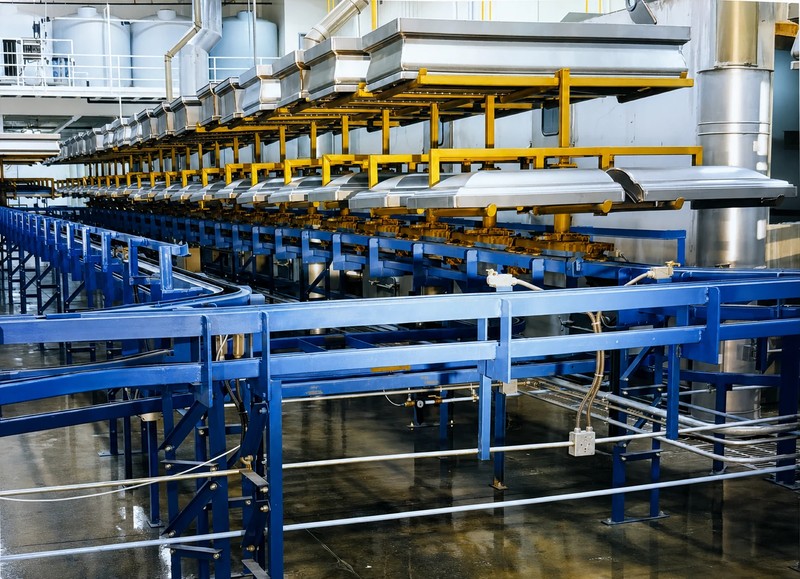 IMH PROJECT / PRODUCTION FLOW & CARRIER SPACING
Rate calculations connect required good parts per shift with process cycle times, available operating time, carrier loading, and equipment capacity. IMH evaluates the flow between operations so the line can be planned around its limiting process.
Required takt is available production time divided by required good-part demand. Specify whether breaks and planned stops are already removed from available time.
For a continuously spaced conveyor, theoretical parts per hour equals 60 × speed in feet per minute × parts per carrier ÷ carrier pitch in feet. Apply appropriate availability and quality assumptions to estimate good output.
Compare each operation’s cycle time, parallel capacity, dwell, and loading constraints. The slowest effective operation limits steady-state output; buffers help absorb variation but do not increase its intrinsic capacity.
Provide target good parts per shift, shift length, planned downtime, carrier pitch and loading, conveyor speed, process dwell, machine cycle times, expected availability, and first-pass yield.
A rate model is only as useful as its assumptions. Validate loading time, part mix, stoppages, changeovers, rework, accumulation, and process requirements. Avoid counting availability losses twice when using measured effective rates.
Share your production goal and site constraints. We’ll work through the engineering scope, equipment interfaces, and path to installation with your team.
Start a project conversation